Industrial refrigeration for prepared meals: optimize your processes
The industry will be well taken care of. Take it from the chef !

Optimize your prepared meals production
The prepared meals industry is evolving rapidly.
We support manufacturers of prepared meals, deli products, cooked vegetables, and plant-based alternatives with high-performance refrigeration and air treatment solutions.
Our expertise guarantees:
- Rigorous control for consistent quality;
- Food safety compliant with regulations;
- Enhanced and eco-efficient energy performance;
Your production deserves technological excellence.
Refrigeration and air treatment for prepared meals plants
Our solutions for prepared meals meet production, quality, and energy efficiency requirements. They combine needs analysis, control of technical parameters, equipment integration, and optimization of operating conditions. This approach allows us to tailor solutions to your site’s processes, volumes, production areas, and priorities.
Our unique expertise combines food safety, energy efficiency and environmental responsibility. This integrated approach transforms your regulatory constraints into competitive advantages.
We support the meat, charcuterie and cured meats industries in their drive towards operational excellence. Our secure, eco-friendly solutions meet the most stringent standards. Industry leaders choose us for this global vision of their production.
Cutting-edge technologies for your performance
Our high-performance equipment transforms your production processes:
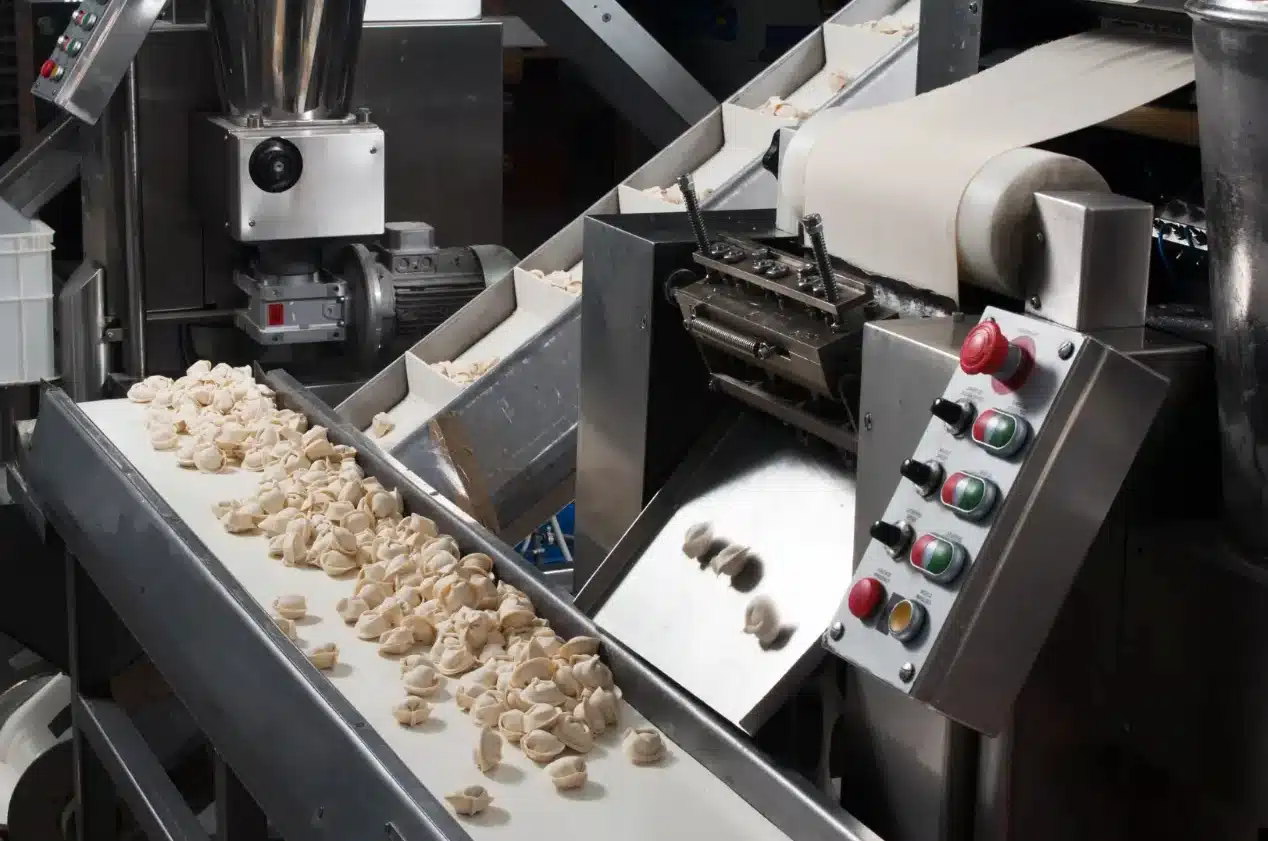
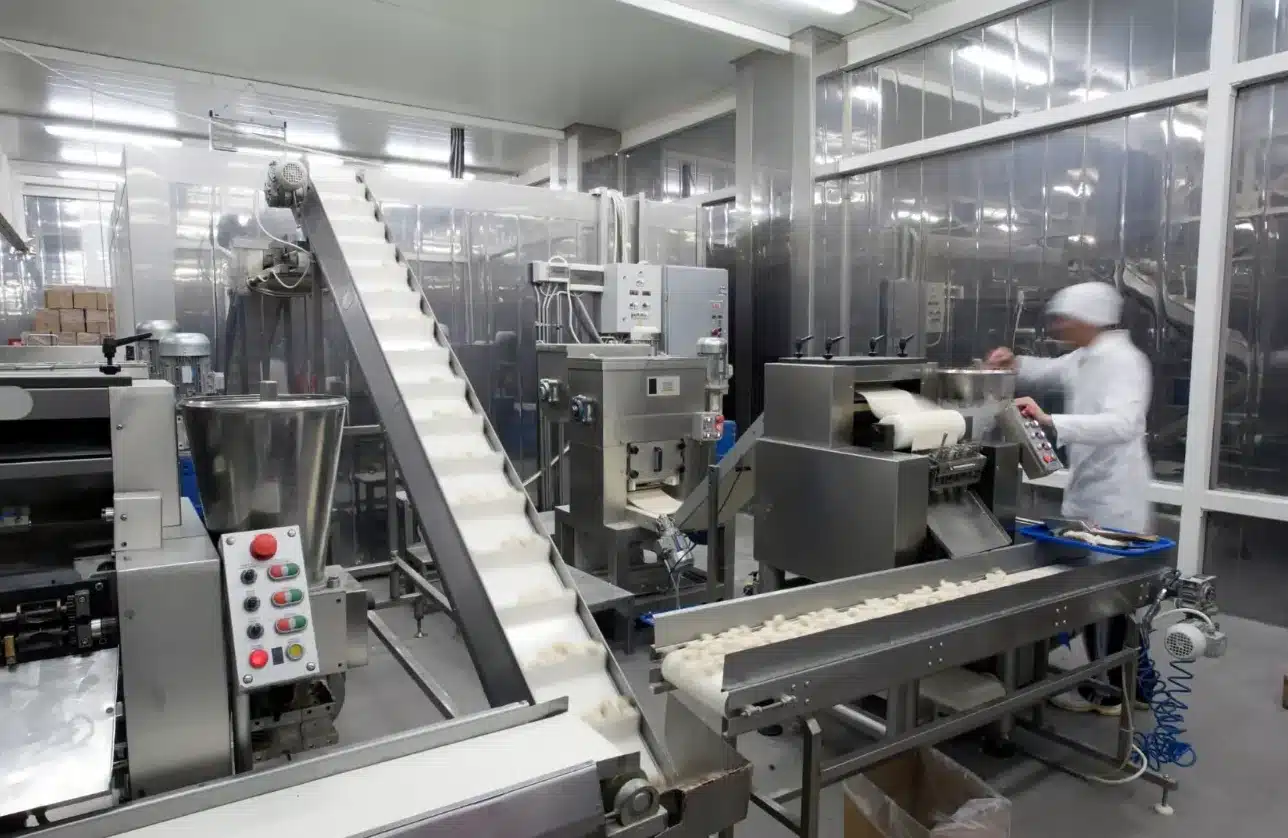
- Stainless steel units and high-speed SMO blast freezing tunnels;
- Next-generation rapid cooling cells;
- Airflow management application for intelligent airflow control;
- MyPortal3E portal with 5-year energy monitoring.
The result: optimized production and a safe work environment for your teams.
Guaranteed standards of excellence for your production
Our solutions meet the highest standards in the food industry.
- Rapid cooling in less than 2 hours.
- Organoleptic qualities preserved. Continuous production 24 hours a day, 7 days a week;
- Maximum guaranteed availability.
- Controlled ultra-clean environments.
- Zero risk of contamination. Strict adherence to your best-before dates;
- Optimized cleaning cycles.
Your production benefits across the board: quality, hygiene, and operational efficiency.
30 years of expertise working toward your future
More than three decades of experience in the prepared meals industry. We have a thorough understanding of your specific production and hygiene requirements.
Our customized solutions are precisely tailored to meet every industrial challenge. High-performance production, impeccable hygienic processes, and an integrated eco-responsible approach.
Leaders in the prepared meals sector trust us for one simple reason: We turn your complex challenges into opportunities for sustainable growth. The plant of tomorrow is being built today, together.
FAQ: practical answers to your operational challenges
The industrial refrigeration challenges faced by prepared meals manufacturers vary depending on their processes, buildings, and production goals. Find answers to the most frequently asked questions to better understand solutions for air treatment, industrial refrigeration, and energy efficiency.
How can industrial refrigeration be optimized for prepared meals?
Industrial refrigeration systems for prepared meals are designed based on the actual on-site conditions: process temperatures, variable loads, production schedules, and building constraints. A properly sized system maintains peak temperatures without consuming excess energy during off-peak periods. Soteck Clauger measures the gap between installed capacity and actual needs, prioritizes corrective actions, and then proposes a solution using natural refrigerants such as NH₃ or CO₂ that is tailored to the objectives of quality, capacity, and reliability.
How can you choose the best cold storage room?
The choice of a cold room depends first and foremost on its intended use: storage of raw materials, curing, preservation of finished products, or a buffer zone prior to shipment. Volume, pallet turnover, the insulation of the outer shell, the doors, and humidity control are just as important as cooling capacity. Before determining the specifications, we verify the actual thermal load, air stratification, and airtightness. This prevents frost buildup and temperature loss when the doors are opened.
How can we optimize the treatment of hygienic air?
Hygienic air treatment protects the product between cooking and packaging, when the risk of recontamination is highest. It relies on filtration, pressure gradients between zones, humidity control, and surfaces that can be thoroughly cleaned. Airflow mapping comes first. It reveals air migration between clean and dirty zones, which we correct before installing stainless-steel air treatment units designed for frequent cleaning.
How can we optimize the blast freezing of prepared meals?
Blast freezing depends on the rate at which the temperature drops, which determines the size of the ice crystals and, therefore, the texture of the product after thawing. The choice between a tunnel, spiral, or plate-type blast freezer depends on the product’s size, thickness, and production rate. Soteck Clauger validates the dwell time, air velocities, and defrost strategy, then connects the equipment to an industrial refrigeration system sized for peak demand.
How can heat recovery be optimized?
The heat rejected by industrial refrigeration condensers is often the cheapest source of energy in a plant. It is used to preheat wash water, process water, or fresh air. However, the heat rejection and the demand must occur simultaneously. We measure the available temperatures and flow rates, verify this simultaneity, and then evaluate the contribution of an industrial heat pump when the temperature is insufficient for the intended use.
How can we optimize the plant’s energy consumption?
In a prepared meals plant, energy consumption is concentrated in refrigeration, air treatment, and hot water systems. Savings rarely come from a single piece of equipment; they result from adjustments to settings, operating schedules, condensing pressure, heat recovery, and continuous monitoring. It all starts with a one-day Flash Audit: we quantify the achievable losses and savings, then identify the Hydro-Québec and Énergir incentives available to fund the selected corrective measures.
How can we optimize equipment upgrades?
Modernizing rather than replacing requires knowing what components are still in good condition. The building envelope, piping, evaporators, and automation systems do not have the same service life as compressors. Converting to natural refrigerants such as NH₃ and CO₂, adding variable-speed drives, and upgrading the control systems often yield the best return on investment. We assess the condition of the equipment and plan the work in phases to minimize production downtime.
How does a prepared meals manufacturer optimize its installations?
A prepared meals manufacturer must adapt to a wide variety of recipes, short production runs, and frequent changes in product size. The installations must adapt to this variability without compromising on temperature or hygiene. Soteck Clauger treats air, refrigeration, and energy efficiency as a single integrated system, makes a contractual commitment to energy performance, and monitors performance through MyPortal3E.
Where should you start when it comes to modernizing your industrial refrigeration system for prepared meals?
It all starts with measurement. We record actual refrigeration loads and hourly profiles. The Flash Audit provides this overview in just one day. It quantifies potential savings and identifies the Hydro-Québec and Énergir incentives available.
A prepared meals manufacturer in Quebec frequently changes its recipes and product formats. The industrial refrigeration system for prepared meals must adapt to this variability. The cold storage room for prepared meals must meet the same requirements. The same applies to the hygienic air treatment system in the industrial kitchen.
Between cooking and packaging, the product remains exposed. Hygienic HVAC systems in the food industry therefore rely on three key factors: filtration, pressure gradients between zones, and humidity control. Airflow mapping comes first. It reveals the movement of air between clean and dirty zones.
In the blast freezing of prepared meals, speed determines texture. Slow cooling results in the formation of large ice crystals. The rapid cooling of foods is determined by the size and rate of the process. The blast freezing of prepared meals is then connected to an NH₃ or CO₂ plant.
The heat rejected by condensers is cheaper than any other form of energy. In the food processing industry, heat recovery involves returning this heat to the wash water. However, the heat rejection and the heat demand must occur simultaneously. This should be verified before making a purchase.
Have our experts evaluate your system. They will calculate the potential savings and then design your industrial refrigeration system for your prepared meals plant. The written performance guarantee covers the targeted results.